Let Us Know How We Can Help. We Are Your Dedicated Solutions Provider.
Global wire harness sourcing is more than comparing unit prices. A small difference in terminal plating, insulation, or crimp height can affect fit, durability, and assembly time. Buyers need clear specifications and suppliers who can explain how they control production.
Quality expert W. Edwards Deming’s well-known reminder, “Quality is everyone’s responsibility,” applies directly to sourcing decisions. It is not a wire-harness-specific quote, but it captures an important point: quality depends on both the supplier’s process and the buyer’s preparation. Ask for test records, material traceability, sample approvals, and realistic production lead times. A tidy presentation is not proof. Evidence matters.
This guide covers ten practical checks, including supplier capability, engineering support, tooling ownership, change control, shipping plans, and total landed cost. Compare like with like. Confirm that drawings, connector part numbers, and acceptance criteria match across quotations. Small details matter. A checklist helps, but it cannot replace a technical review or a frank conversation with the factory. Even experienced buyers can miss a detail when schedules tighten. That is worth admitting. A dependable wire harness partner should answer specific questions clearly, flag risks early, and support consistent quality from prototype through repeat orders.
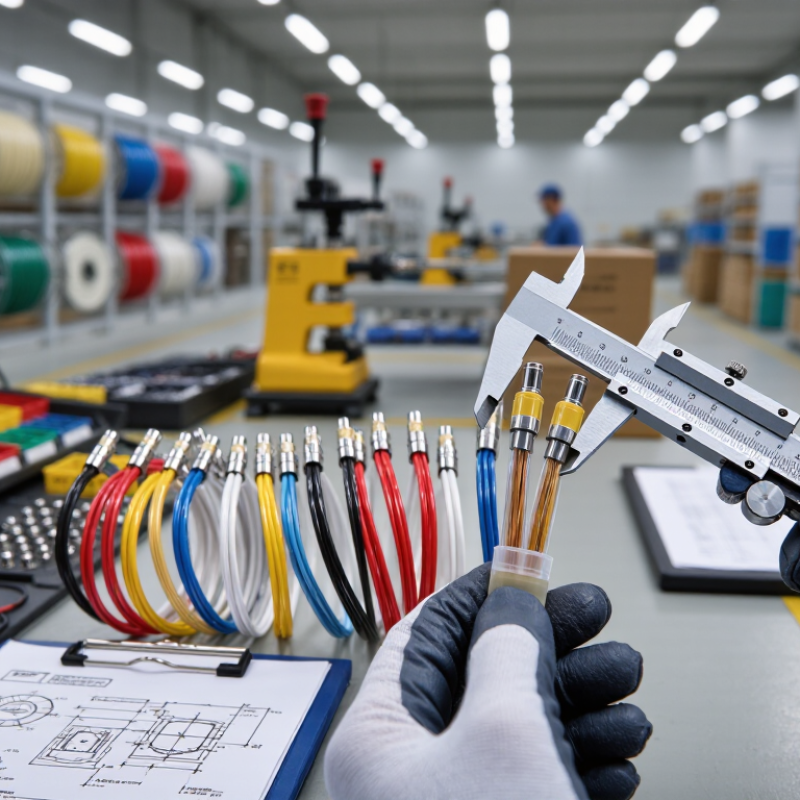
Understanding wire harness requirements starts with the equipment, not a catalog. List each circuit’s voltage, expected current, and operating cycle. A motor that starts repeatedly may need different sizing than a steady sensor circuit. Small details matter. Record wire gauge, insulation type, color, and required length before requesting quotations.
Next, study the harness’s actual route through the product. Measure bends, clearances, and branch points, including space needed for clips and connector access. Check exposure to heat, vibration, moisture, oils, or abrasion. These conditions influence material and protection choices. A harness that fits a drawing may still be difficult to install. Measure twice.
Specify connector types, pin assignments, labeling, and any testing requirements. Share clear drawings and revision numbers so suppliers are not working from conflicting files. For unusual routing or tight spaces, a physical sample can reveal problems that a drawing misses. It may feel slower at first, but correcting connector access before production is usually easier than reworking finished assemblies. Some requirements will change after the first build; note those changes promptly and verify the updated design against the real application.
Typical nominal voltage levels vary by application, from 12 V passenger-car systems to 400 V and 800 V electric-vehicle traction architectures. These are common reference levels, not universal specifications; confirm voltage, current, environment, and compliance requirements against the project’s technical specification.
Wire-harness sourcing starts with a drawing that specifies more than length and connector type. Define each circuit’s current, voltage, temperature range, and routing environment. Include wire gauge, insulation material, color, shielding, and allowable voltage drop. A harness near an engine needs different insulation and abrasion protection from one inside a dry control cabinet. Small details matter.
Material planning also deserves attention. The USGS Mineral Commodity Summaries 2025 estimated global copper mine production at about 23 million metric tons in 2024. That scale does not guarantee stable lead times or prices for a particular wire grade. Ask suppliers to identify conductor composition, insulation specifications, and approved material substitutions. Put substitutions in writing. A tidy drawing can still leave room for costly interpretation.
Set measurable acceptance criteria before requesting quotations. Reference applicable workmanship and test methods, such as IPC/WHMA-A-620 and IEC 60512, where suitable. Specify continuity, insulation resistance, crimp dimensions, pull-force testing, and inspection records. For a crimp, request actual measurements, not only a pass label. Define sampling frequency and corrective-action expectations, too. I have seen specifications focus heavily on components while overlooking test evidence; that gap is easy to miss. Require a sample build and review its routing, labels, and connector fit before approving production.
Evaluating a global wire harness supplier means checking more than price and a polished capability deck. Ask which processes are performed in-house, from wire cutting and stripping to crimping, overmolding, and electrical testing. Then compare those claims with production records, equipment lists, and a live factory review. Details matter: can the supplier show calibrated pull-test equipment and identify the lot used for each sample?
Request a small pilot run before committing to volume. Review connector fit, label readability, continuity results, and variation between operators or shifts. Ask how capacity changes during peak demand, and whether key materials have qualified alternatives. A supplier may quote a short lead time, but confirm what it assumes about tooling, approvals, and shipping. Time zones complicate follow-up. Set clear response windows and name one technical contact on each side. Language gaps can also hide small drawing changes, so record revisions in writing.
Certifications help, but they do not prove consistent execution on your specific assembly. Compare audit findings with corrective-action evidence, not just a certificate date. I have seen supplier scorecards overvalue equipment counts; a newer machine does not guarantee stable crimp height. Leave room for a second review after the first production batch. That extra check can feel slow. It may prevent a costly surprise.
Wire-harness quotes can look comparable while hiding different costs. Check copper, terminals, connector availability, tooling, inspection, packaging, and freight separately. A low unit price may depend on a large order or long replenishment cycle. Ask suppliers to show assumptions, not just the final number. A spreadsheet can still miss the cost of a line stoppage.
Tips: Compare landed cost at the same delivery point, order quantity, and payment terms. Request lead times for materials, production, testing, and transport as separate figures. Ask what happens if a connector or terminal arrives late. One missing part can hold up a finished harness.
The World Bank’s 2023 Logistics Performance Index reports an average of 44 days for shipments to travel from an exporter’s warehouse to an importer’s. Actual transit times vary widely. UNCTAD’s Review of Maritime Transport 2024 also describes shipping disruptions and longer routes that can affect schedules and freight costs. Build a modest buffer for critical parts, and map where key materials come from. I would not trust one promised date. Recheck it against recent delivery records and current capacity.
| # | Sourcing Tip | What to Compare | Typical Cost Effect | Lead-Time Effect | Supply Chain Risk | Practical Buyer Action |
|---|---|---|---|---|---|---|
| 1 | Compare total landed cost, not just the unit price | Harness price, tooling, packaging, freight, duties, insurance, inspection, and inventory carrying costs | May reveal that a lower quoted price has higher delivered cost | Freight mode and border processing can change the delivery schedule | Hidden charges or customs delays can disrupt budgets and deliveries | Request an itemized quotation with delivery terms, currency, and assumptions clearly stated |
| 2 | Standardize the technical specification before requesting bids | Drawings, bill of materials, wire gauge, insulation, terminals, tolerances, labeling, and test requirements | Clear specifications reduce quote gaps and avoid unplanned engineering changes | Fewer clarification rounds can shorten the quotation and approval process | Ambiguous requirements can lead to nonconforming parts or rework | Issue the same controlled specification and revision to every bidder |
| 3 | Check material origin and availability | Availability and approved alternatives for wire, terminals, connectors, seals, and protective coverings | Substitutions or constrained materials may change the price | Specialty or allocation-constrained components can extend production schedules | Dependence on a single material source increases disruption exposure | Ask suppliers to identify critical components, origin, and approved substitutes before award |
| 4 | Evaluate production capacity and order flexibility | Available labor, equipment, current loading, minimum order quantities, and ability to handle demand changes | Small batches may carry higher per-unit setup costs | Overloaded lines or inflexible production slots can delay replenishment | Capacity constraints can affect multiple orders at once | Request a capacity plan, realistic monthly output, and procedures for urgent changes |
| 5 | Validate quality systems and process controls | Traceability, incoming inspection, crimp monitoring, continuity testing, calibration, and nonconformance handling | Stronger controls may add inspection cost but help prevent scrap and field failures | Inspection and corrective action can affect release timing | Weak process control raises the risk of defects reaching assembly or end users | Review sample records and audit the processes relevant to the harness design and risk level |
| 6 | Confirm validation requirements and ownership | Prototype approval, electrical tests, dimensional checks, environmental testing, and responsibility for test fixtures | Testing and fixtures can add upfront costs | Unplanned validation can delay production release | Unclear acceptance criteria can cause disputes or repeated testing | Agree on a written validation plan, acceptance limits, sample quantities, and approval milestones |
| 7 | Compare logistics routes and delivery terms | Transit mode, shipment frequency, consolidation, customs responsibilities, insurance, and delivery location | Air freight is generally more expensive than ocean or consolidated ground transport | Air is typically faster; ocean and consolidated shipments usually require more transit planning | Port congestion, border issues, and route disruption can affect arrival dates | Compare door-to-door options and build realistic transit and customs buffers into the schedule |
| 8 | Assess geographic concentration and contingency plans | Factory location, upstream component concentration, alternate production sites, and recovery arrangements | Maintaining a backup source may increase qualification and administrative costs | Switching production requires time for tooling, samples, and approval | Regional disruptions can affect suppliers that share the same upstream sources | Map critical dependencies and document a practical recovery or alternate-source plan |
| 9 | Agree on forecast, inventory, and change-control rules | Forecast horizon, order commitment window, safety stock, cancellation terms, and engineering-change process | Inventory buffers tie up working capital; frequent changes can create obsolete stock | Stable forecasts improve material planning and production scheduling | Forecast volatility can cause shortages, excess inventory, or missed delivery dates | Define forecast updates, firm-order periods, inventory ownership, and revision approvals in writing |
| 10 | Use a balanced supplier scorecard and review performance | Delivered cost, on-time delivery, defect trends, responsiveness, corrective actions, and financial or operational resilience | Choosing only the lowest bid may overlook costs from delays and quality issues | Consistent performance data helps identify schedule risks earlier | Unmonitored supplier deterioration can go unnoticed until deliveries are affected | Track agreed metrics regularly and review corrective actions and continuity plans with the supplier |
Comparison note: Cost and lead-time effects are directional planning considerations, not guaranteed outcomes. Actual results depend on harness complexity, material availability, order volume, shipping route, customs requirements, and the agreed delivery terms.
Tip: Define compliance requirements before requesting quotes. Confirm the destination market, applicable standards, labeling, and documentation with qualified compliance staff. Ask suppliers for current material declarations and process records, not just a certificate. Requirements can vary by product and market. A tidy spreadsheet may still miss a drawing revision, so assign one person to control document versions.
Tip: Share a controlled drawing, bill of materials, and clear acceptance criteria. Specify wire gauge, insulation, color codes, terminal details, and permitted tolerances. Check production capacity against your forecast, then approve a representative sample before volume runs. Small changes matter. A substitute terminal may fit but perform differently under vibration. Record approved changes in writing, even when schedules feel tight.
Tip: Build inspection into the production plan. Review incoming material records, crimp dimensions, continuity results, and sample pull-test data. Agree on sampling levels and defect handling before the first shipment. Keep lot traceability practical and readable. For delivery, confirm lead times, packaging, shipping documents, and buffer stock. Moisture protection may be useful for long routes. Even a careful plan can miss a small revision, so recheck critical details before dispatch.